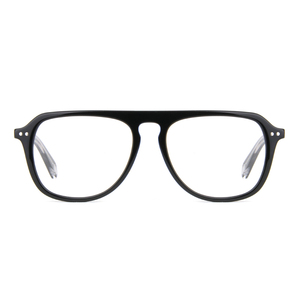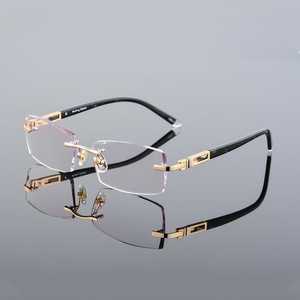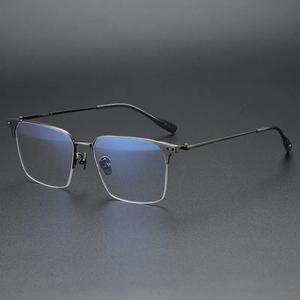
Sourcing Guides
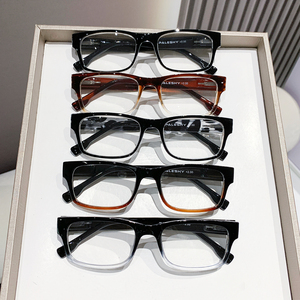
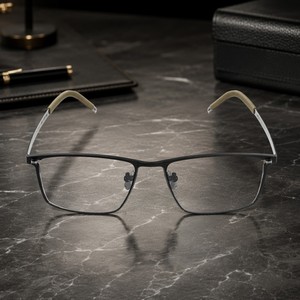
wholesale optical frames acetate optical frames wholesale tortoiseshell acetate frames cellulose acetate spectacle frames hand-finished acetate eyeglasses rectangle acetate optical frames square acetate optical frames titanium optical frames wholesale Global Service Top SearchCompany
About Elistro Dealer Program ContactOur flagship lightweight spectacle silhouettes are manufactured using sub-millimeter CNC micro-milling, hand-finished tumbling barrels, and vacuum ion plating (IP). Designed to provide optical labs with flawless cold-glazing stability while ensuring sub-15g ergonomic wear for end patients.
Selecting optical chassis raw materials dictates laboratory lens edging yield, patient bridge comfort, and multi-year after-sales hinge stability. Our factory implements direct traceability on all titanium billets and bio-cellulose slabs to meet strict ANSI Z80.5 and EN ISO 12870 standards.
| Material Classification | Specific Density (g/cm³) | Tensile Strength (MPa) | Flexural Elastic Memory | Hypoallergenic Rating | Optimal Optical Application |
|---|---|---|---|---|---|
| Japanese Pure Titanium (Gr. 2) | 4.51 (Ultra-Light) | 480 – 550 | Rigid Geometric Integrity | 100% Bio-compatible (Nickel-Free) | High-index prescription bridges, minimalist rimless luxury mountings. |
| Aerospace Beta-Titanium (β-Ti) | 4.75 | 1050 – 1200 | Dynamic Ultra-Flex (90° bend memory) | 100% Bio-compatible (Nickel-Free) | Pressure-free flex temples, active lifestyle eyewear, screwless hinges. |
| Aged Cellulose Acetate (3.5–4mm) | 1.28 | 90 – 110 | Thermo-formable adjustment memory | Certified Skin-Safe (Bio-Cellulose) | Bespoke designer optical frames, deep bevels for high minus (-8.00D) lenses. |
| Swiss EMS Grilamid TR90 | 1.02 (Floats near water) | 65 – 85 | Extreme Impact & Low-Temp Memory | Non-cytotoxic / Food Grade | High-volume enterprise readers, pediatric frames, safety computer eyewear. |
| Surgical Stainless Steel (304L/316L) | 7.95 | 600 – 750 | Moderate Spring Return | Passivated Anti-Nickel Release | Ultra-thin sheet metal chassis, architectural cutaways, cost-efficient bulk OEM. |
As consumer behavior converges on digital ergonomics, sustainability compliance, and bespoke facial sizing, eyewear importers and brand directors must adjust purchasing strategies across the following four market developments.
Remote digital work habits have escalated chronic temporal headache and nasal compression complaints. Retail opticians report an 82% higher customer close rate for frames weighing under 12 grams. Sourcing portfolios are shifting heavily toward featherweight Beta-Titanium and high-density micro-milled acetate.
EU green taxonomy regulations and conscious consumer sentiment demand bio-based plasticizers (diethyl phthalate replacement). Leading retail chains require factory-level verification of biodegradable acetate flakes alongside Closed-Loop Water Scrubbing during tumble-polishing manufacturing phases.
High capital lockups in legacy 1,000-piece single-color orders have given way to modular OEM partnerships. Brands demand flexible production lines offering 100-to-300 unit MOQ allocations per SKU across diversified colorways, supported by rapid CNC custom mold prototyping within 14 days.
Distributors are cutting localized repackaging overheads by outsourcing full consumer packaging downstream to the factory. Sourcing contracts increasingly demand integrated, pre-branded 5-piece packaging suites (cases, hard boxes, microfiber cloths, warranty credentials) drop-shipped directly to regional hubs.
Our manufacturing facility incorporates German CNC robotics, automated laser soldering, and precision barrel polishing techniques to overcome traditional durability limitations in lightweight eyewear design.
Legacy mechanical stamping introduces internal stress vectors that cause spontaneous rim warpage during laboratory lens cold-insertion. By deploying 5-axis robotic CAD/CNC milling down to ±0.03mm tolerances, our frame fronts ensure exact bevel grove alignment and seamless high-cylinder Rx lens fitting.
Over 68% of post-purchase consumer warranty claims stem from loose or stripped temple screws. Our R&D engineering department has pioneered friction-driven, screwless cam-hinge mechanisms that pass 25,000 continuous open-close flex cycles without torque degradation or joint loosening.
Traditional wet electroplating degrades quickly when exposed to aggressive human perspiration and cosmetic chemicals. We utilize high-vacuum Physical Vapor Deposition (PVD) to fuse titanium nitride layers at 0.3-micron depths, guaranteeing zero corrosion and passing 48-hour artificial sweat immersion testing.
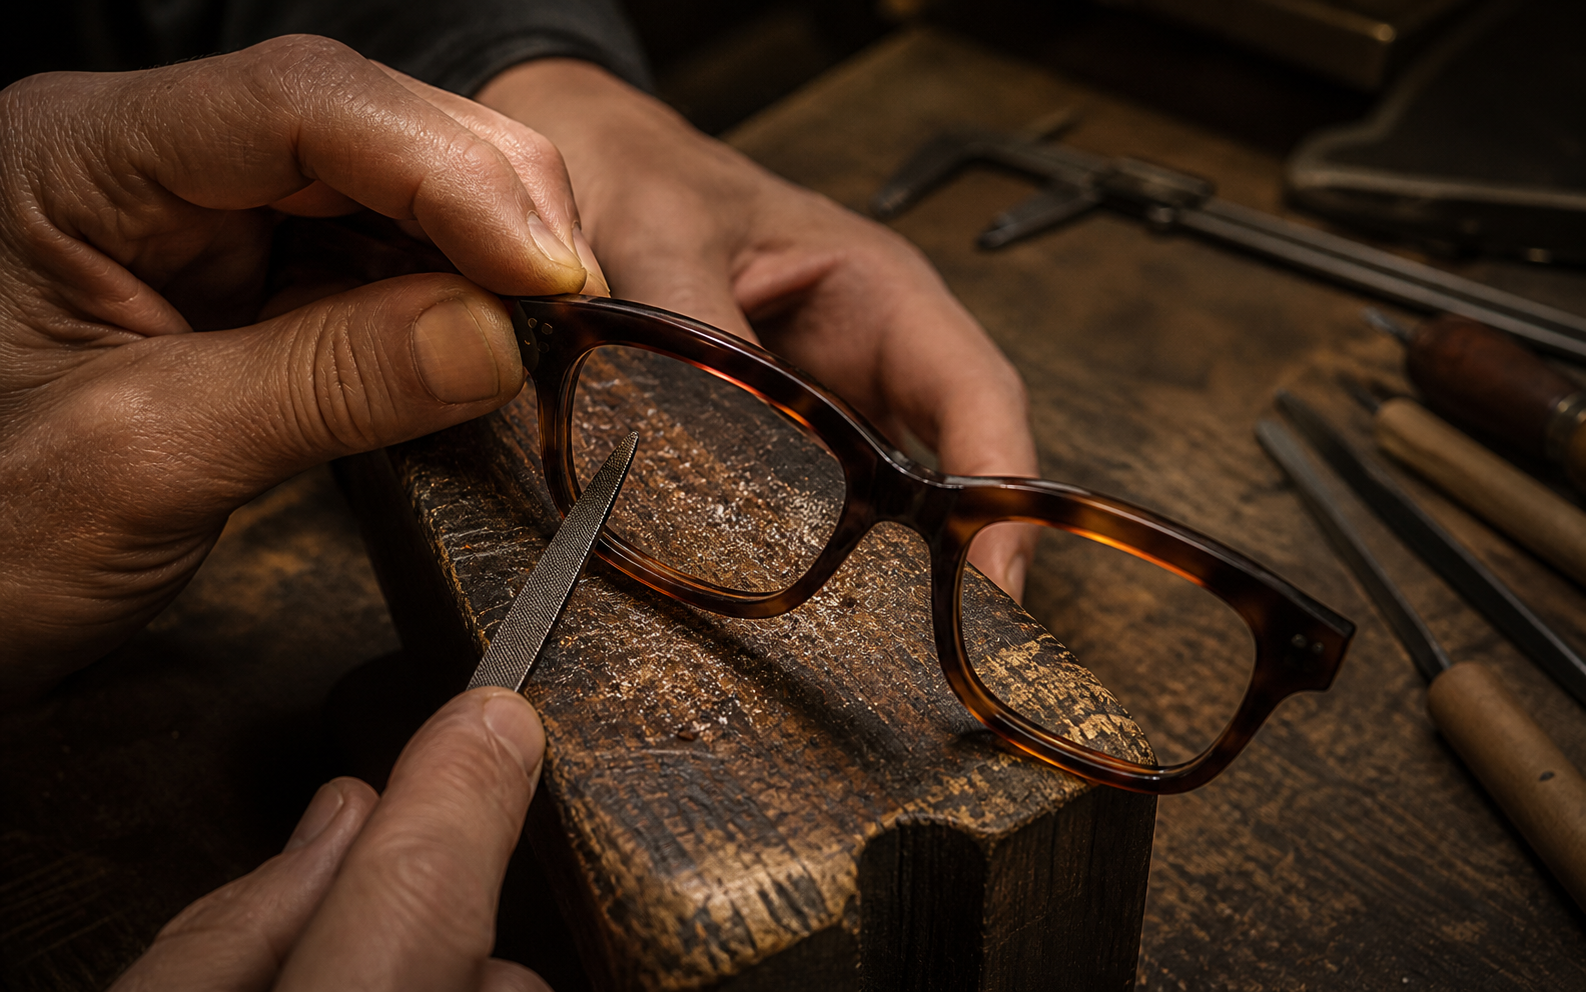
While automated CNC machines deliver structural precision, premium eyewear achieves tactile perfection only through human touch. Every frame passing through our manufacturing bays undergoes hand profile shaping, bridge alignment, manual temple pin set-ins, and three distinct stages of organic walnut shell tumbling.
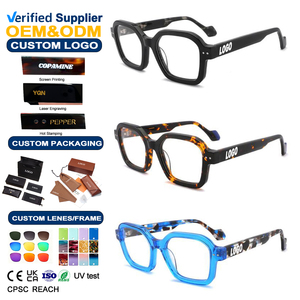
From initial rapid 3D CAD design prototyping to custom laser logo engraving, our OEM/ODM infrastructure empowers eyewear retail brands to launch shelf-ready collections in under 45 days.
Elevate your customer unboxing experience and command higher retail optical margins without spending internal resources managing separate packaging suppliers. Every production order can be configured with your custom brand logo applied across our comprehensive 5-piece luxury kit.
Heavyweight textured paper bag with reinforced cotton handles.
Matte-coated presentation box with foil embossed brand stamping.
Impact-resistant ergonomic case with soft-touch inner velvet lining.
High-density 220 GSM non-abrasive optical lens cleaning cloth.
Serialized certificate card verifying material purity and UV grade.
Direct answers to the engineering, compliance, financial, and logistical questions commonly evaluated during supplier qualification and factory audit reviews.
For existing catalog models with custom private-label laser engraving, our flexible MOQ begins at 100 pieces per model (divided across up to 3 stock colorways). For full bespoke OEM development requiring custom tooling, mold fabrication, and exclusive acetate sheet laminations, our baseline run is 300 pieces per design silhouette.
We machine optical eye-wires with a standardized 0.8mm deep V-groove angled at precisely 115°. This geometry supports automated laboratory edgers during lens mounting. Our pure titanium and beta-titanium retain strict tensile balance, ensuring zero lens cracking or flaking during high diopter (-6.00 to -10.00D) prescription installations.
Our manufacturing and QC protocols comply directly with ISO 12870:2016 (Ophthalmic optics — Spectacle frames). Furthermore, our metal and acetate frames pass the EN 16128 nickel release test, meet European CE conformity directives, and are listed under US FDA Medical Device Class I regulations for ophthalmic frames.
Rapid 3D CAD modeling and resin concept samples are rendered within 72 hours. Precision-milled metal or acetate physical samples require 12 to 15 working days. Full mass-production cycles typically average 35 to 50 days depending on the complexity of electroplating or custom acetate curing requirements.
Rather than relying on low-grade liquid chemical spray finishes, we utilize multi-chamber Vacuum Ion Plating (IP) alongside cathodic Physical Vapor Deposition (PVD). This process anchors metal particles at an atomic scale, passing the 48-hour artificial sweat immersion test and ensuring hypoallergenic contact for sensitive skin.
Yes. Our in-house optical engineering team routinely translates hand sketches, physical samples, or mood boards into production-ready 2D mechanical drawings and 3D STP/IGES files. We compute facial ergonomic distribution, bridge clearance, and pantoscopic tilt calculations prior to mold fabrication.
We execute an AQL 1.0/2.5 inspection standard across four production checkpoints: Incoming Raw Material Spectrometry, In-Process CNC Milling Checks, 24-Hour Barrel Tumble Polish Audit, and 100% Pre-Packaging Mechanical Alignment (including temple closing torque, bridge plane symmetry, and hinge tension).
Absolutely. We use cured cellulose acetate cured for at least 60 days to stabilize plasticizer density. This prevents post-manufacture warping while allowing dispensing opticians to easily heat, curve, and contour end-pieces and temples using standard hot-air bench warmers without milky whitening or surface pitting.
Connect with our technical optical sales engineering team today to review our comprehensive wholesale SKU lineup, verify custom tooling quotes, and request physical sample boxes for your optical retail network.