Sourcing Guides
wholesale optical frames acetate optical frames wholesale tortoiseshell acetate frames cellulose acetate spectacle frames hand-finished acetate eyeglasses rectangle acetate optical frames square acetate optical frames titanium optical frames wholesale Global Service Top SearchCompany
About Elistro Dealer Program ContactDirect B2B OEM/ODM manufacturing solutions compliant with CE, ANSI Z80.5, and ISO 12870 standards. Fully customizable configurations for independent chains and multinational eyewear brands.
Combining traditional artisan craftsmanship with high-precision CNC tooling, cleanroom galvanic plating, and rigorous quality assurance.
Production environments certified under ISO 9001:2015 and ISO 13485 (Class I Medical Spectacle Frames). REACH & FDA registration ready.
Monthly production output exceeding 450,000 completed optical frames across 6 specialized production lines with 99.4% on-schedule dispatch.
Proprietary Physical Vapor Deposition (PVD) titanium ion plating delivering surface hardness above 2500 Vickers and 96-hour salt-spray resistance.
CAD-to-physical prototype iteration in 7 days via high-precision SLA 3D printing and 5-axis micro-milling prior to production tooling.
A comprehensive analysis for optical chain buyers, category managers, and retail chain procurement teams.
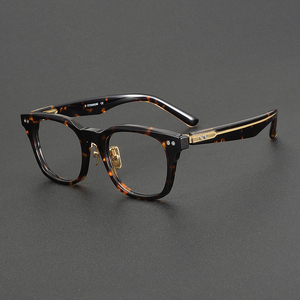
Traditional petroleum-derived cellulose acetate (cellulose diacetate plasticized with DEP/DMP) is rapidly phased out in tier-1 retail markets. Next-generation European and Japanese flake raw material uses non-phthalate bio-based plasticizers derived from citric acid esters. These formulations preserve tensile strength above 48 MPa while offering enhanced dimensional stability under elevated dispensing bench temperatures up to 80°C.
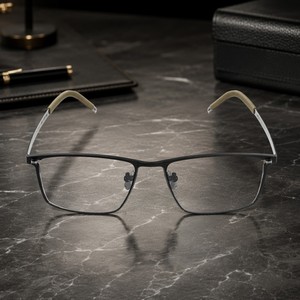
Precision aerospace beta-titanium wire (Ti-15V-3Cr-3Sn-3Al) provides high yield-strength-to-modulus ratios, allowing ultra-thin 0.8mm rim wires and self-adjusting temple arms without mechanical work hardening. Combined with micro-welding in inert argon chambers, joint rupture resistance exceeds 250N, mitigating bridge snapped bridge returns under standard optical clinic lens edging procedures.
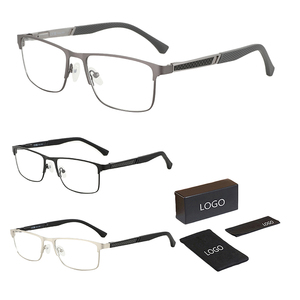
Modern professional men demand minimal front weight without structural flexion. By sandwiching 3K unidirectional carbon fiber prepreg sheets between dual 0.6mm acetate layers under high-pressure autoclaving (0.8 MPa at 135°C), the resulting frame front exhibits negligible torsional warp, ensuring high cylinder prescription lenses stay positioned precisely at their calculated optical axes.
| Mechanical & Operational Metric | Milled Cellulose Acetate | Pure / Beta-Titanium | Carbon Fiber Composite | Memory Polymer (TR90) |
|---|---|---|---|---|
| Density / Weight Ratio | 1.28 - 1.32 g/cm³ (Substantial) | 4.51 g/cm³ (Extremely Light Profile) | 1.55 g/cm³ (Featherweight Rigidity) | 1.14 g/cm³ (Ultralight Floating) |
| Dispensing Adjustability | Direct heat frame warmer (65°C-75°C) | Cold bend pliers with nylon jaws | Preset ergonomics (Internal wire-core) | Cold bend with temple core-wire |
| Corrosion & Salt Sweat Immunity | High (Periodic buffing required) | 100% Bio-inert / Zero Oxidation | Inert / Chemically Impervious | High Resistance to cosmetic solvents |
| Lens Edging Groove Stability | Standard V-groove / High base curve | Rimless screw / Nylon rim-lock wire | Precision CNC micro-bevel groove | Standard optical bevel locking |
| Recommended End-User Target | Executive, architectural, fashion-led | Clinical, corporate, ultra-extended wear | High-performance, tech professionals | Active lifestyle, digital office reading |
Strategic procurement considerations shaping retail order specifications, sustainability mandates, and end-consumer demand patterns.
European supply chain regulations now mandate documented chain-of-custody data for raw acetate and metal ores. Leading global brands require frame manufacturers to demonstrate acetate milling waste reclamation (converting scrap cuttings into recycled black acetate sheets) alongside waterless tumbling and ultrasonic wash systems.
Traditional chassis are evolving to support modular hardware integrations. OEM requests increasingly call for hollow-core temple channels (minimum 2.2mm internal diameter) engineered to accommodate capacitive touch sensors, micro-transducers, and low-profile battery cells without sacrificing front frame balance.
Standardized sizing is yielding to targeted demographic fits. Western fittings typically require narrower bridges (16–18mm) with deep crest angles, whereas Asian and Hispanic anatomical designs feature elevated, molded splay-angle nose pads (20–22mm) with reduced pantoscopic tilt angles (6° vs. standard 10°–12°).
Key operational and engineering considerations answered by our chief optical production engineers.
Standard cellulose acetate OEM manufacturing requires 300 units per model, supporting up to 3 distinct colorways (100 units/color). Pure and Beta-Titanium styles maintain an MOQ of 300 units due to custom stamping dies and dedicated vacuum PVD batch setups. In-stock ready-ship models from our export catalogue accommodate trial distributor orders from 50 units per SKU.
We exclusively integrate custom CNC-machined 5-barrel and 7-barrel hinges with Teflon-coated or thread-locked Nylok screws. Every production lot undergoes automated pneumatic hinge open/close testing, requiring zero structural play or screw displacement over 25,000 cycles under a 15-degree lateral load.
Yes. We offer fiber-optic micro-laser engraving inside temple arms, hot-foil core-wire foil stamping, high-resolution pad printing, and custom titanium end-piece cast insignias. All laser applications comply with ISO 12870 visibility and depth standards to prevent skin irritation or premature sweat erosion.
Consignments pass a 4-tier inspection protocol: (1) Raw acetate moisture equilibrium stabilization for 72 hours; (2) CNC dimensional checks against CAD drawings within ±0.05mm tolerances; (3) Multi-axis frame alignment checks on optical calibration granite slabs; and (4) 100% manual surface finishing and hinge-torque auditing.
Rapid 3D printed fit samples ship within 5-7 business days. Fully finished functional prototypes from pilot tooling require 20-25 days. Mass industrial production requires 45-60 days for acetate frames and 60-70 days for pure titanium lines, including full salt-spray and nickel-release laboratory testing.
We provide unified turnkey packaging manufacturing, including custom-molded vegan leather hard cases, dual-surface 220gsm microfiber cleaning cloths, high-density magnetic gift boxes, anti-counterfeit guarantee cards, and FSC-certified retail shopping bags configured to your brand identity.
Consult with our structural eyewear engineers, access our complete 2026/2027 export catalog, and request physical material swatches for your brand.
Send an Inquiry